Overview
Industrial Reactors
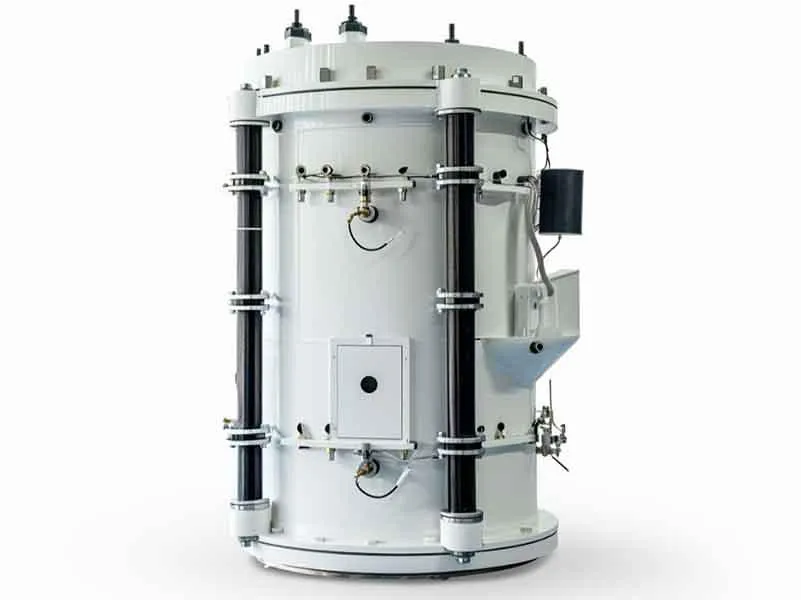
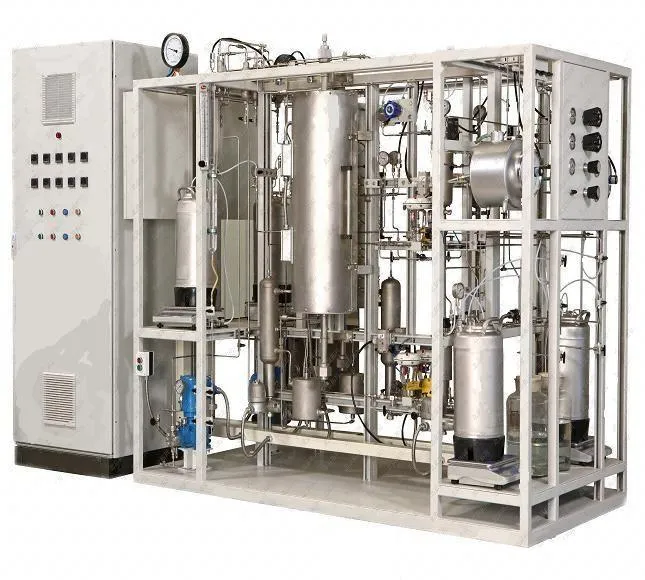
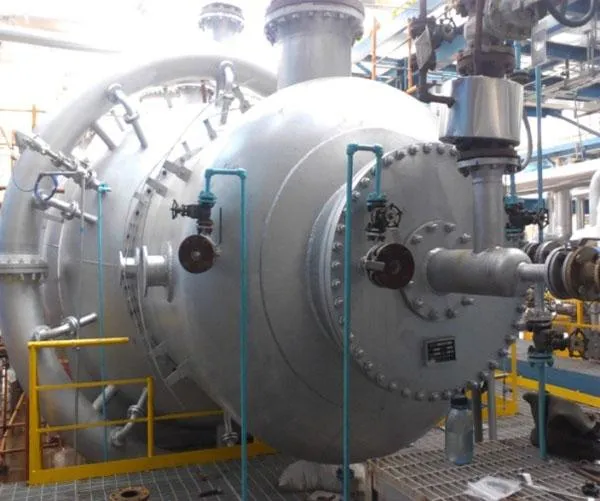
Our reactor portfolio covers different configurations and process technologies, addressing a variety of reaction requirements across industrial facilities.
High Reliability
Energy Efficiency
Flexible Design
Global Standards
Product Range
Our Industrial Reactors Range
Jacketed Reactors
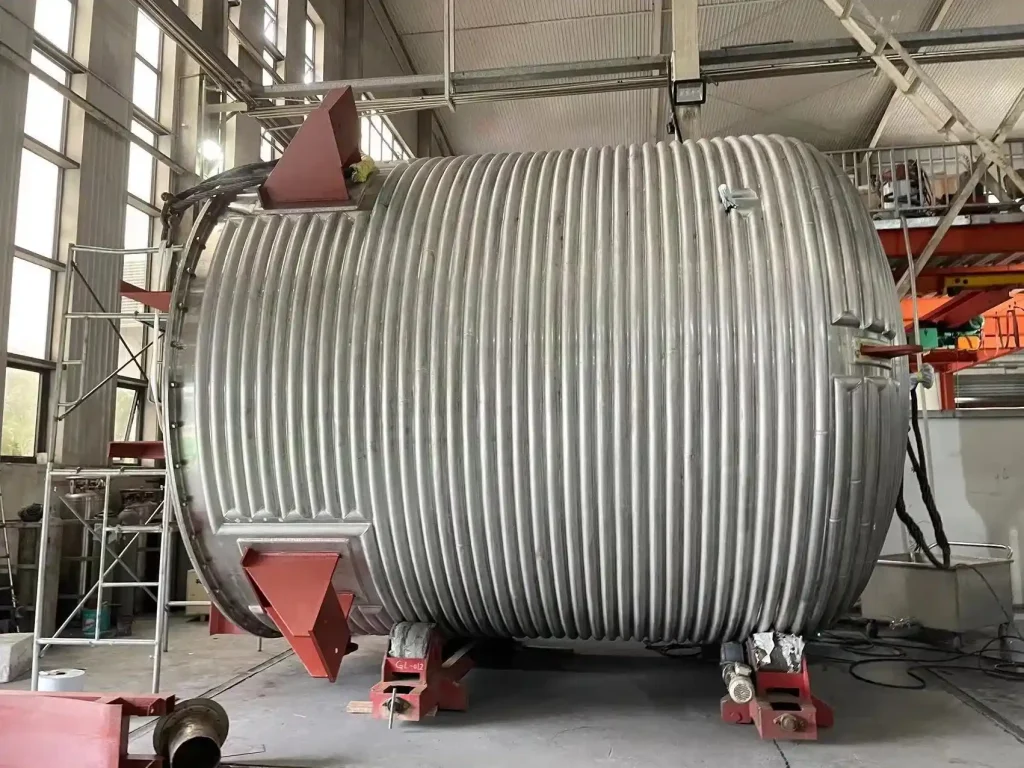
Half-Coil Reactors
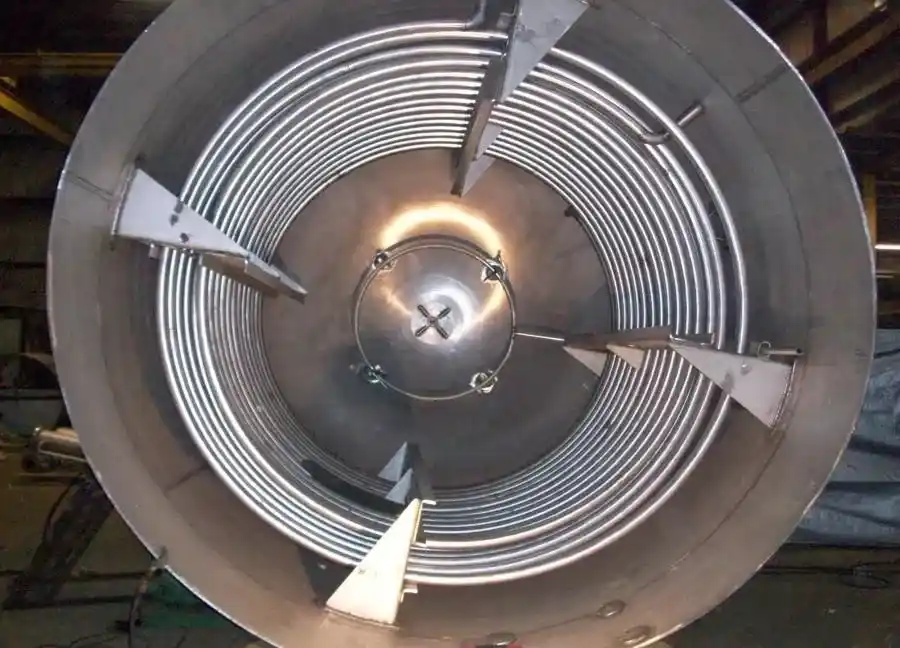
Coil Reactors
Continuous Stirred-Tank Reactors (CSTR)
Fixed-Bed Reactors
Trickle-Bed Reactors
Fluidized-Bed Reactors
Claus Reactors
TGTU Reactors
Oxidation Reactors
Reformers
Featured Product
Joint
Venture
Products
- Advanced Process Control
- High Operational Efficiency
- Corrosion-Resistant Materials
- High-Pressure & Temperature Resistance
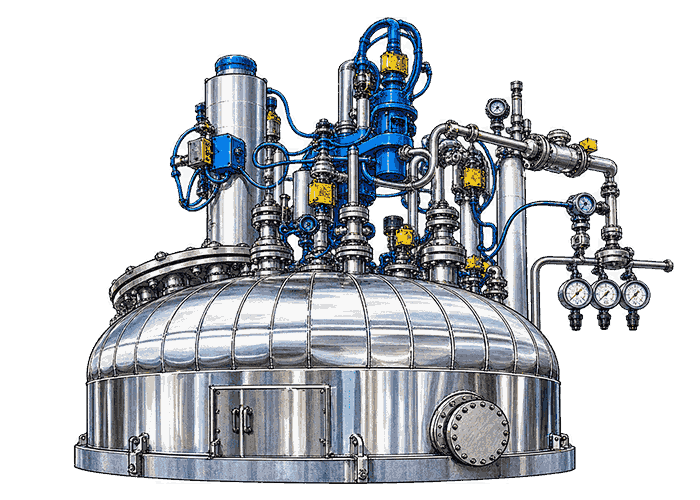
The available range includes stirred-tank, jacketed, coil, fixed-bed, fluidized-bed and specialized process reactors.
Advanced Industrial Reactor Engineering Solutions
PEM provides engineered industrial reactor solutions designed to support a wide range of chemical processing and industrial production applications. Our reactor systems are developed to meet demanding process requirements, ensuring reliable operation, efficient process control and long-term equipment performance.
Combining engineering expertise, mechanical design capabilities and industrial equipment integration, PEM delivers reactor solutions tailored to specific operating conditions, process characteristics and project specifications.
Our approach focuses on developing reliable equipment that supports complex industrial processes while maintaining high standards of quality, safety and operational efficiency.
Engineered for Reliable Process Performance
Industrial reactors are essential equipment in chemical and petrochemical facilities, where controlled chemical reactions are required to transform raw materials into valuable products.
PEM’s industrial reactor solutions are designed to accommodate different process conditions, including operating pressure, temperature, reaction requirements and material compatibility. These systems can be engineered for various industrial applications, including chemical processing, petrochemical production, refining and other process industries.
Our engineering approach emphasizes mechanical integrity, process requirements, material selection and equipment integration to ensure dependable performance in demanding industrial environments.
Industrial Reactor Types & Applications
PEM provides reactor solutions designed to support different industrial processes and operating requirements:
Pressure Reactors – Designed for chemical reactions under controlled pressure and temperature conditions.
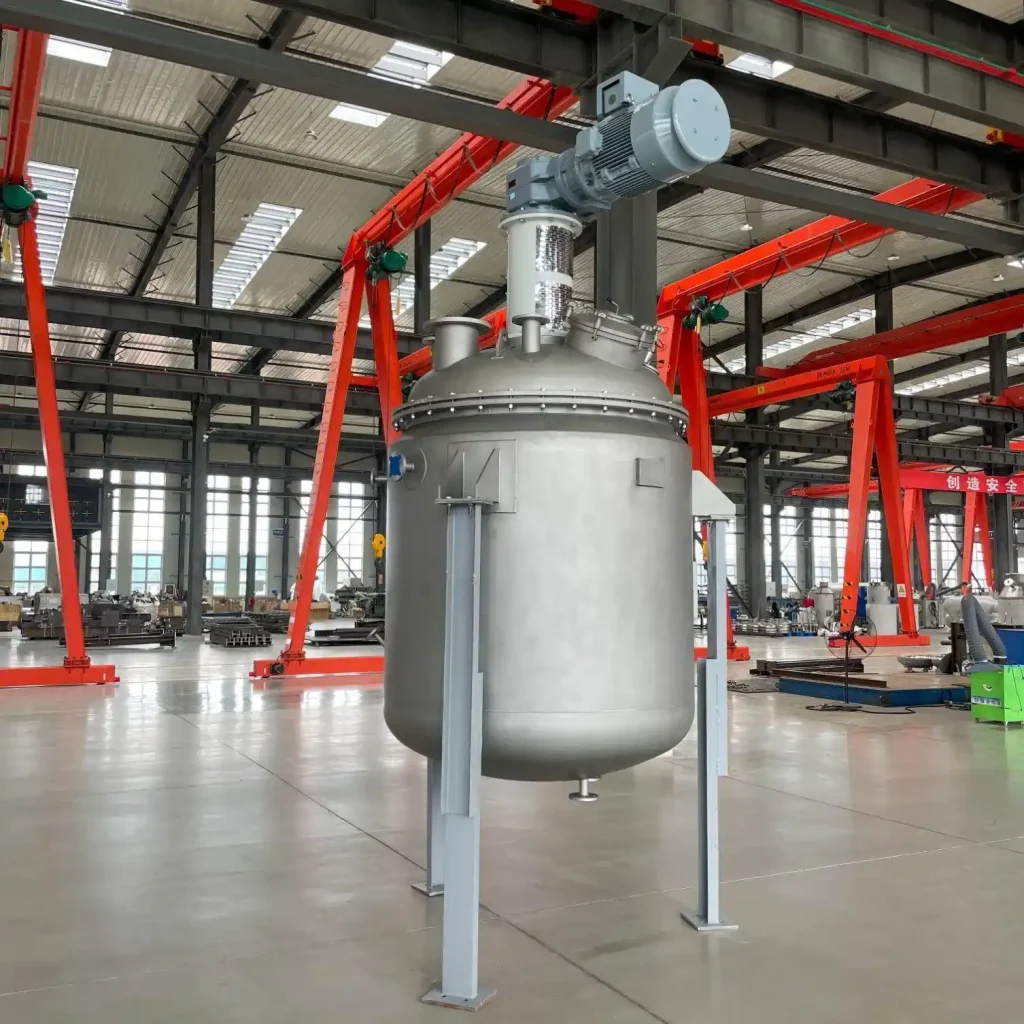
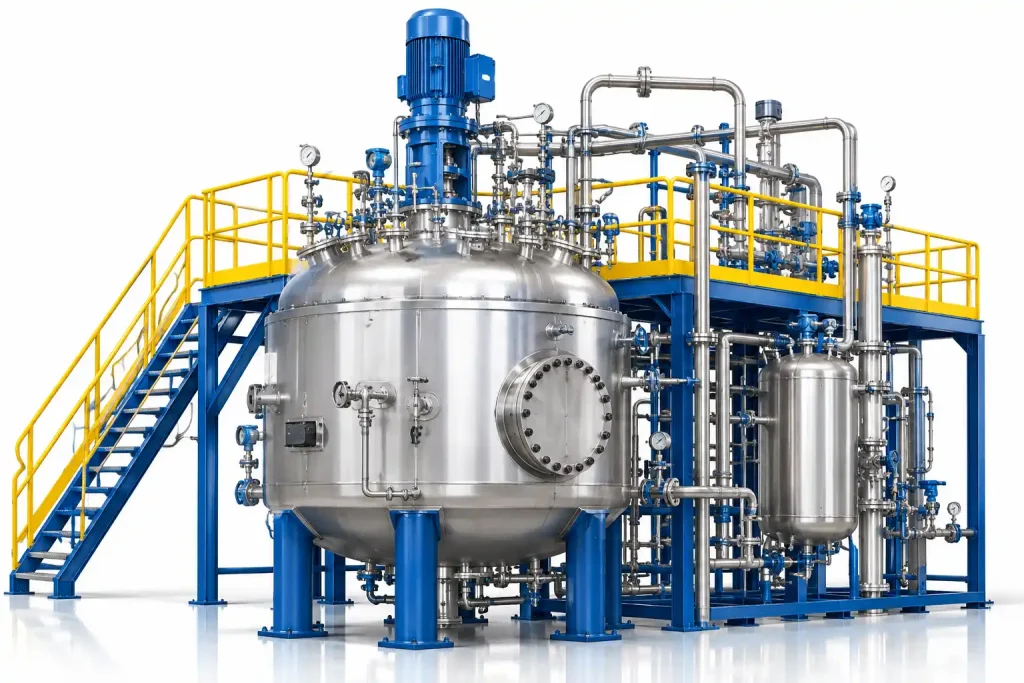
Stirred Tank Reactors – Equipped with mixing systems to support uniform reaction conditions and efficient process operations.
Jacketed Reactors – Designed for precise temperature control through integrated heating and cooling systems.
Fixed Bed Reactors – Used in catalytic processes where reactants pass through a stationary catalyst bed.
Custom-Designed Reactors – Engineered according to specific process requirements, operating conditions and project specifications.
Each reactor configuration is developed with consideration for process performance, mechanical design, material compatibility and long-term operational reliability.
Why Choose PEM
Engineering Excellence for Your Industrial Needs
With decades of experience and a strong commitment to quality, PEM delivers advanced boiler solutions backed by global standards and industry expertise.